Sheet-Fed vs Roll-Fed Paper Bag Machine: How Each One Works
In one sentence: it converts paper — either a continuous roll or pre-printed sheets — into finished bags through a fixed sequence of forming steps: feeding, tube forming, cutting, bottom folding, gluing and delivery, all synchronized by servo motors and a central PLC. A modern roll-fed machine completes the entire sequence in under two seconds per bag.
This sheet-fed vs roll-fed paper bag machine comparison walks through every stage of the process for the two machine families — roll-fed and sheet-fed — and explains the components that decide whether a machine runs reliably at speed. If you are comparing machines to buy, understanding these steps is what lets you read a spec sheet critically.
The process at a glance
- Feeding — paper roll unwinds (roll-fed) or printed sheets feed in one by one (sheet-fed)
- Printing — optional inline flexo printing on roll-fed lines
- Tube forming — paper is folded around a former and glued into a continuous tube
- Gusset folding — side folds are creased so the bag can expand
- Cutting — the tube is cut to individual bag lengths
- Bottom forming — the base is opened, folded and glued (square/SOS or V-bottom)
- Handle attachment — twisted or flat handles applied inline, where equipped
- Delivery — finished bags are counted and stacked
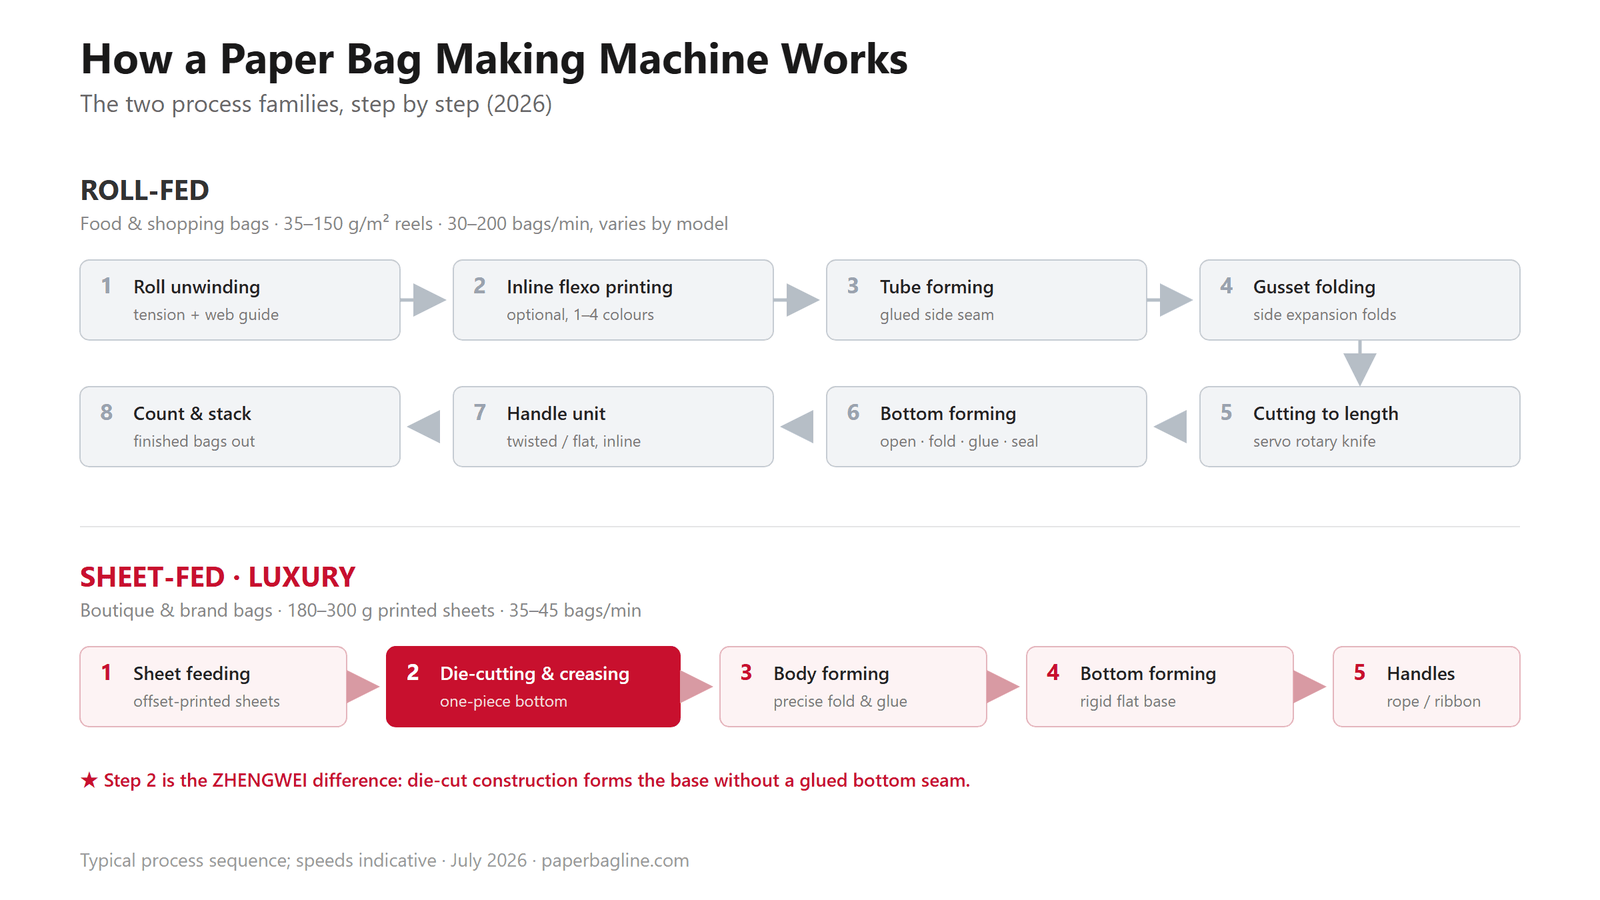
How a roll-fed paper bag making machine works, step by step
Step 1: Unwinding and web guiding
A kraft paper reel mounts on an unwind stand with automatic tension control. A web guide system keeps the paper edge running perfectly straight; without it, every downstream fold would drift. On better machines, tension and guiding are servo-controlled rather than mechanical, which is what allows clean running at high speed with thin paper.
Roll-fed machines as a class run paper from about 35 to 150 g/m², but no single model covers that whole span. Buyers who plan around the headline range often find their paper sits outside the model they were actually quoted.
Step 2: Inline printing (optional)
Many roll-fed lines include one- to four-colour flexo printing units that print the web before forming. Print quality is adequate for grocery and food-service bags; it is not comparable to offset printing, which matters later when we get to luxury bags.
Printing also costs speed. Frames with an inline print unit typically top out somewhere between 100 and 150 bags per minute, depending on the model and the bag width, against up to 200 on unprinted frames. The print unit sits between the handle cut-off and the patch attachment, which is why printing frames are also longer and draw far more power.
Step 3: Gluing and tube forming
Glue is applied along one edge, and the flat web is folded around a forming plate into a continuous tube. This glued overlap becomes the side seam — present on standard and luxury bags alike, so it is not what separates them. The construction difference that does separate them appears two steps later, at the bottom of the bag.
This stage depends on the web being held under steady tension. Any flutter in the web can put the glue bead out of line, and a bead laid too thin is a common reason a bag splits under load after it has been packed.
Step 4: Gusset folding
Side gussets — the accordion folds that let a bag expand — are creased into the tube by folding wheels. Gusset depth is one of the parameters that sets a machine’s bag size range.
Step 5: Cutting
A rotating knife cuts the tube into individual bag lengths, either straight or serrated. Cut length is set on the touchscreen and executed by servo — on modern machines, changing bag length is a parameter change, not a mechanical rebuild.
Cut length is not bag height, and the difference catches buyers out. On a narrow frame the cut length might run 190–370 mm, but a 370 mm cut does not give you a 370 mm bag: part of that length is consumed further down the line building the bottom. A machine can cover the bag width you need and still not reach the bag height you need, so check both.
Step 6: Bottom opening, folding and gluing
The most mechanically complex station. Vacuum grippers open the tube end, forming fingers fold the base — square (SOS) or V-bottom — glue is applied in a precise pattern, and press rollers seal it. This is what leaves a bonded seam running across the base of a conventional bag. Bottom quality is where cheap and well-built machines visibly differ: a poorly glued base is the most common field failure of budget machines.
Step 7: Handle attachment (where equipped)
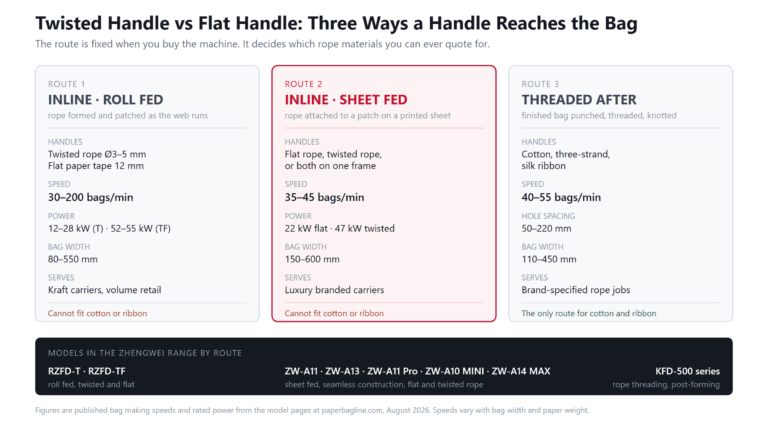
Machines with inline handle units make twisted or flat paper handles from separate paper rolls, glue them to patches, and press the patches onto the bag — all synchronized with the main line. An inline handle unit is effectively a second machine bolted to the first, which is why it adds so much to the machine price.
A handle also raises the paper floor, the minimum weight of stock the job needs. On roll-fed frames the practical floor rises to around 80 g/m² once a handle unit is fitted, so a bag that runs unhandled on light kraft may not run handled on the same paper.
Step 8: Counting and delivery
Finished bags are counted photoelectrically and delivered in stacks, ready for packing. Roll-fed output runs from about 30 up to 200 bags per minute depending on bag size and model; flat-bottom food-bag frames, which carry no handle station, reach 580.
Sheet-fed vs roll-fed paper bag machine: how the sheet-fed process differs
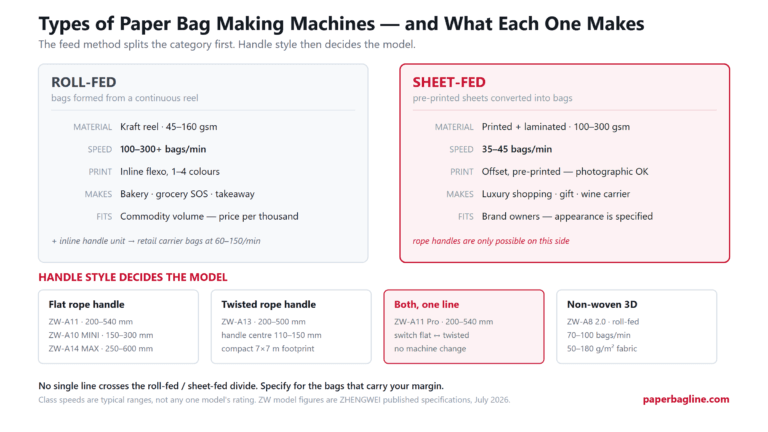
So how does a paper bag making machine work when the product is a luxury bag? Everything above describes tube-forming from a continuous roll. Luxury shopping bags — the rigid, offset-printed, rope-handled bags used in fashion and cosmetics retail — are made the other way around, starting from pre-printed sheets of board (180–300 g on ZHENGWEI’s range), often laminated or surface-finished.
The sheet-fed sequence: printed sheets feed in one at a time → each sheet is creased and cut to the bag’s exact geometry → formed into the bag body → the base is folded and glued → handles (rope or ribbon) are attached. Because printing happens on an offset press before the bag machine, print quality is limited only by the print shop, not the bag line.
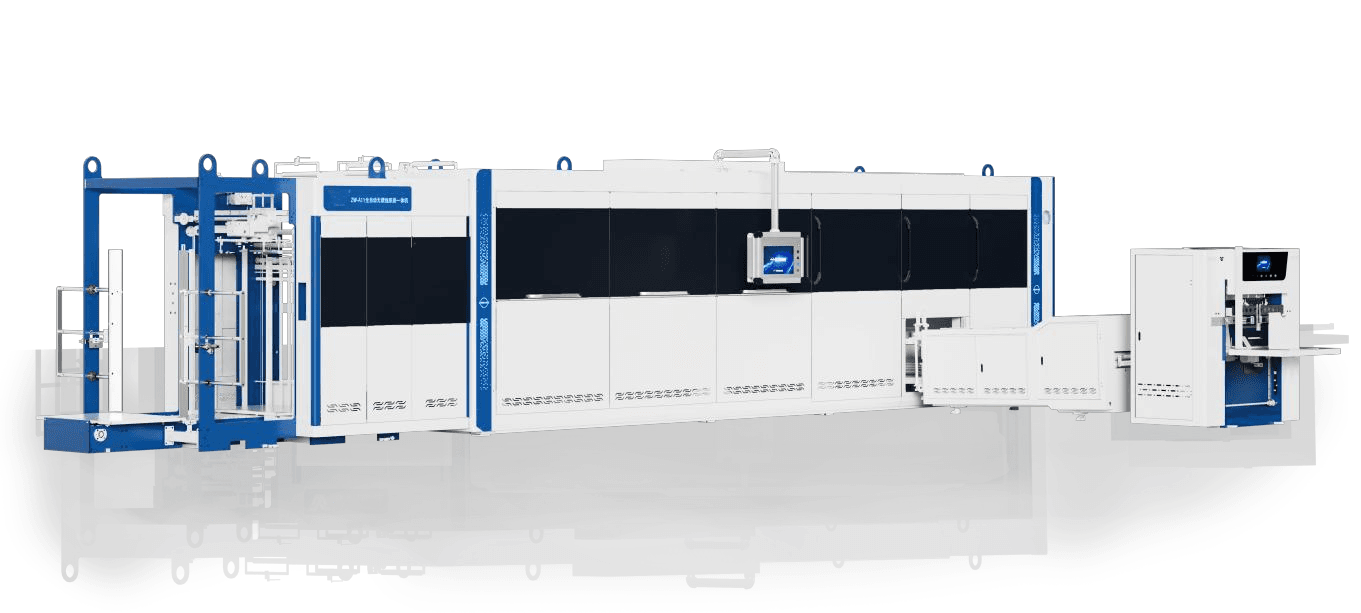
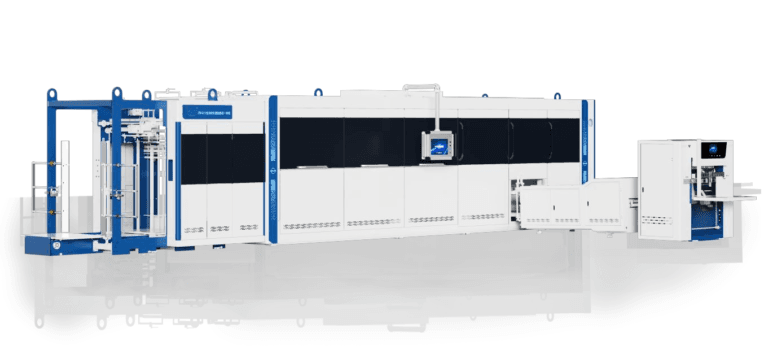
Within the sheet-fed category there is one further construction difference, and it is at the base. Conventional sheet-fed machines fold the bottom inward and glue it shut, exactly like a roll-fed tube — leaving a bonded seam across the base. Die-cutting-based seamless machines — the technology our ZW series is built on — wrap a die-cut blank in a U around the base, so the bottom is one continuous piece of paper with no bottom seam at all; the joins sit at the two side folds instead. On a bag that sells retail identity, that base is the difference customers can see and feel every time they set the bag down; the construction comparison is covered in detail in our seamless vs traditional guide.
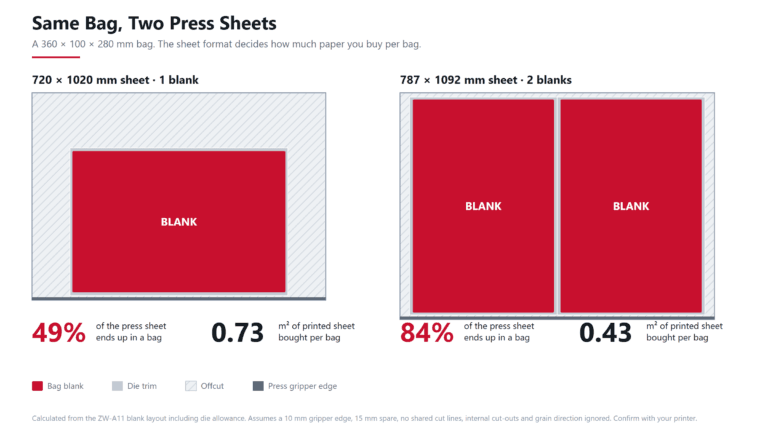
Tip: Check your artwork against the sheet size range before you look at anything else. The ZW-A11 takes sheets 560–1040 mm long and 310–680 mm wide. A design that falls outside that cannot run, no matter what the bag width and height columns say. This is the specification buyers check last and regret first.
The components that decide reliability
- Servo motors synchronize every station electronically. More servo axes = faster changeovers and more precise registration; mechanical-linkage machines are cheaper and slower to adjust.
- PLC and touchscreen hold bag recipes. Look for mainstream brands (Siemens, Mitsubishi, Schneider) — the control platform determines whether spare parts exist in 10 years.
- Vacuum and pneumatic systems do the physical gripping and folding; component brand (SMC, Festo) is a good proxy for overall build honesty.
- Glue systems — cold water-based glue for bodies and bottoms, hot-melt on some handle units. Nozzle-based application is cleaner and more adjustable than wheel-based.
- Photocells and registration sensors keep printed designs aligned with cuts and folds — the difference between a centred logo and scrap.
What wears first
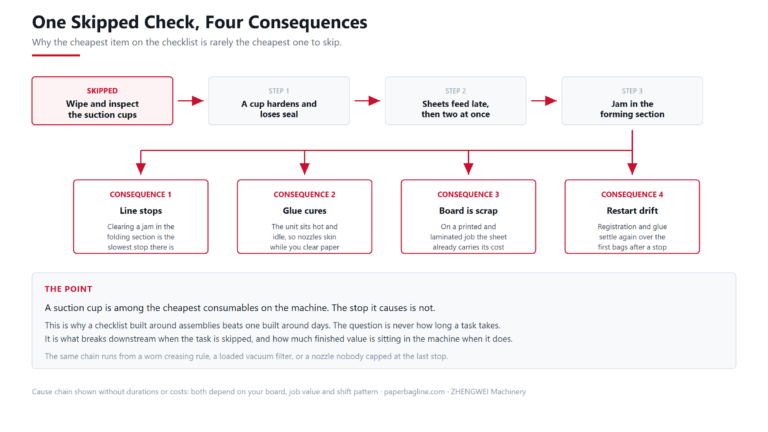
Those components decide how a machine is built. Day to day, three parts decide whether it keeps running: the suction cups on the feeder, the glue nozzles, and the creasing rule.
Suction cups. A hardened or split cup does not announce itself at the feeder. It shows up later as a jam in the folding section, which is why the link between the two is worth knowing. ZHENGWEI’s service schedule calls for wiping the cups every shift and testing suction at least once a week.
Glue nozzles. Nozzles should be purged and capped at every stop, and soaked and flushed at least once a week. A skinned nozzle, where stagnant adhesive has partly blocked it, is a common cause of a base that opens under heavy load.
Creasing rule. If the steel creasing rule wears shallow it stops striking cleanly. The crease is not properly formed, and the bag will not fold as it should further down the line.
Tip: Bring your own board to the factory visit and ask them to run it. Machines are demonstrated on stock the supplier chose, and recycled or heavier board does not always behave the same way. Seeing your own material run is worth more than any figure in a brochure.
Speed, staffing and material in practice
- Output: semi-automatic machines produce roughly 80–1,000 bags per hour; roll-fed automatics run about 30–200 bags per minute, varying by model; sheet-fed luxury lines run slower — around 40–45 bags per minute — because bag construction is heavier and more precise.
- Staffing: a fully automatic line typically needs 2–3 operators for loading, quality checks and packing, and that figure does not rise with the number of bags produced.
- Material: roll-fed machines handle kraft and coated papers of roughly 35–150 g/m² across the class; sheet-fed machines handle printed and laminated board, 180–300 g on ZHENGWEI’s range.
Read the bottom of a quoted speed range as the realistic operating point. A 550 mm bag on a wide roll-fed frame rated 30–110 bags per minute runs much closer to 30 than to 110; the top of the range belongs to the easiest job the machine can do, not necessarily to yours.
Tip: Decide your material class before you shortlist machines. Sheet-fed machines take 180–300 g board and do not run paper from a reel. A thin kraft grocery bag at 35–80 g/m² is a roll-fed job, and no sheet-fed machine on any shortlist will make it. Ask a supplier which of their ranges your paper actually belongs to before you compare anything else.
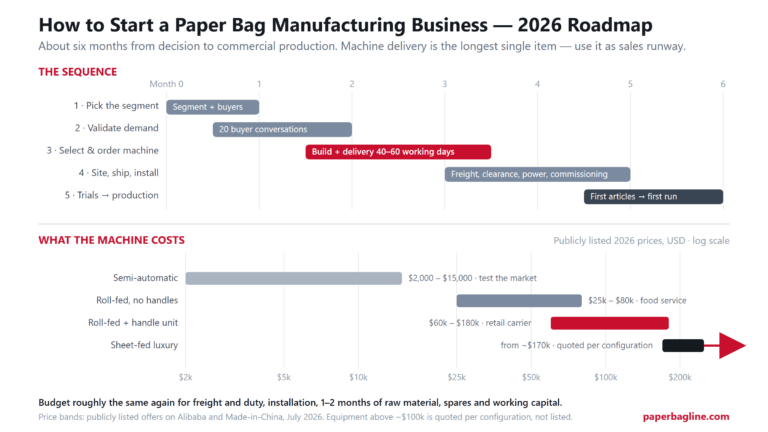
How these numbers translate into machine budgets is covered in our 2026 price guide, and how to match machine class to your product is in the selection guide.
FAQ: How Does a Paper Bag Making Machine Work in Practice?
How many bags per minute can a paper bag making machine produce?
Roll-fed automatic machines produce about 30–200 bags per minute depending on bag size and model, and flat-bottom food-bag frames reach 580. Sheet-fed luxury machines run around 40–45 bags per minute, and semi-automatic machines manage roughly 80–1,000 bags per hour.
How many workers does a paper bag making machine need?
A fully automatic machine typically runs with 2–3 operators handling material loading, quality inspection and packing. Semi-automatic production needs significantly more labour per bag because handles and finishing are manual.
What paper can a paper bag machine use?
Roll-fed machines process kraft, white and coated papers from reels, roughly 35–150 g/m² across the class. Sheet-fed machines process offset-printed and laminated sheets, 180–300 g on ZHENGWEI’s range, — the material class luxury bags are made from.
What is the difference between roll-fed and sheet-fed machines?
Roll-fed machines form bags from a continuous paper roll at high speed with inline flexo printing — ideal for food and grocery bags. Sheet-fed machines form bags from pre-printed sheets at lower speed but far higher print and finish quality — the only way to produce true luxury bags.
Why do some machine-made bags have no bottom seam?
Standard machines fold the base of the bag inward and glue it shut, which always leaves a bonded seam running across the bottom. Seamless machines wrap a die-cut blank in a U around the base instead, so the bottom is a single continuous piece of paper with no seam at all — a construction currently available on ZHENGWEI’s sheet-fed ZW series.
Want to see the process on a real machine? Send us your bag specification and we will produce free sample bags on the exact ZW model that fits it — with a detailed quotation within 24 hours. Explore our five seamless sheet-fed machines or contact our engineering team.